
Feeder — Bulk channel
Bulk channel (C1)
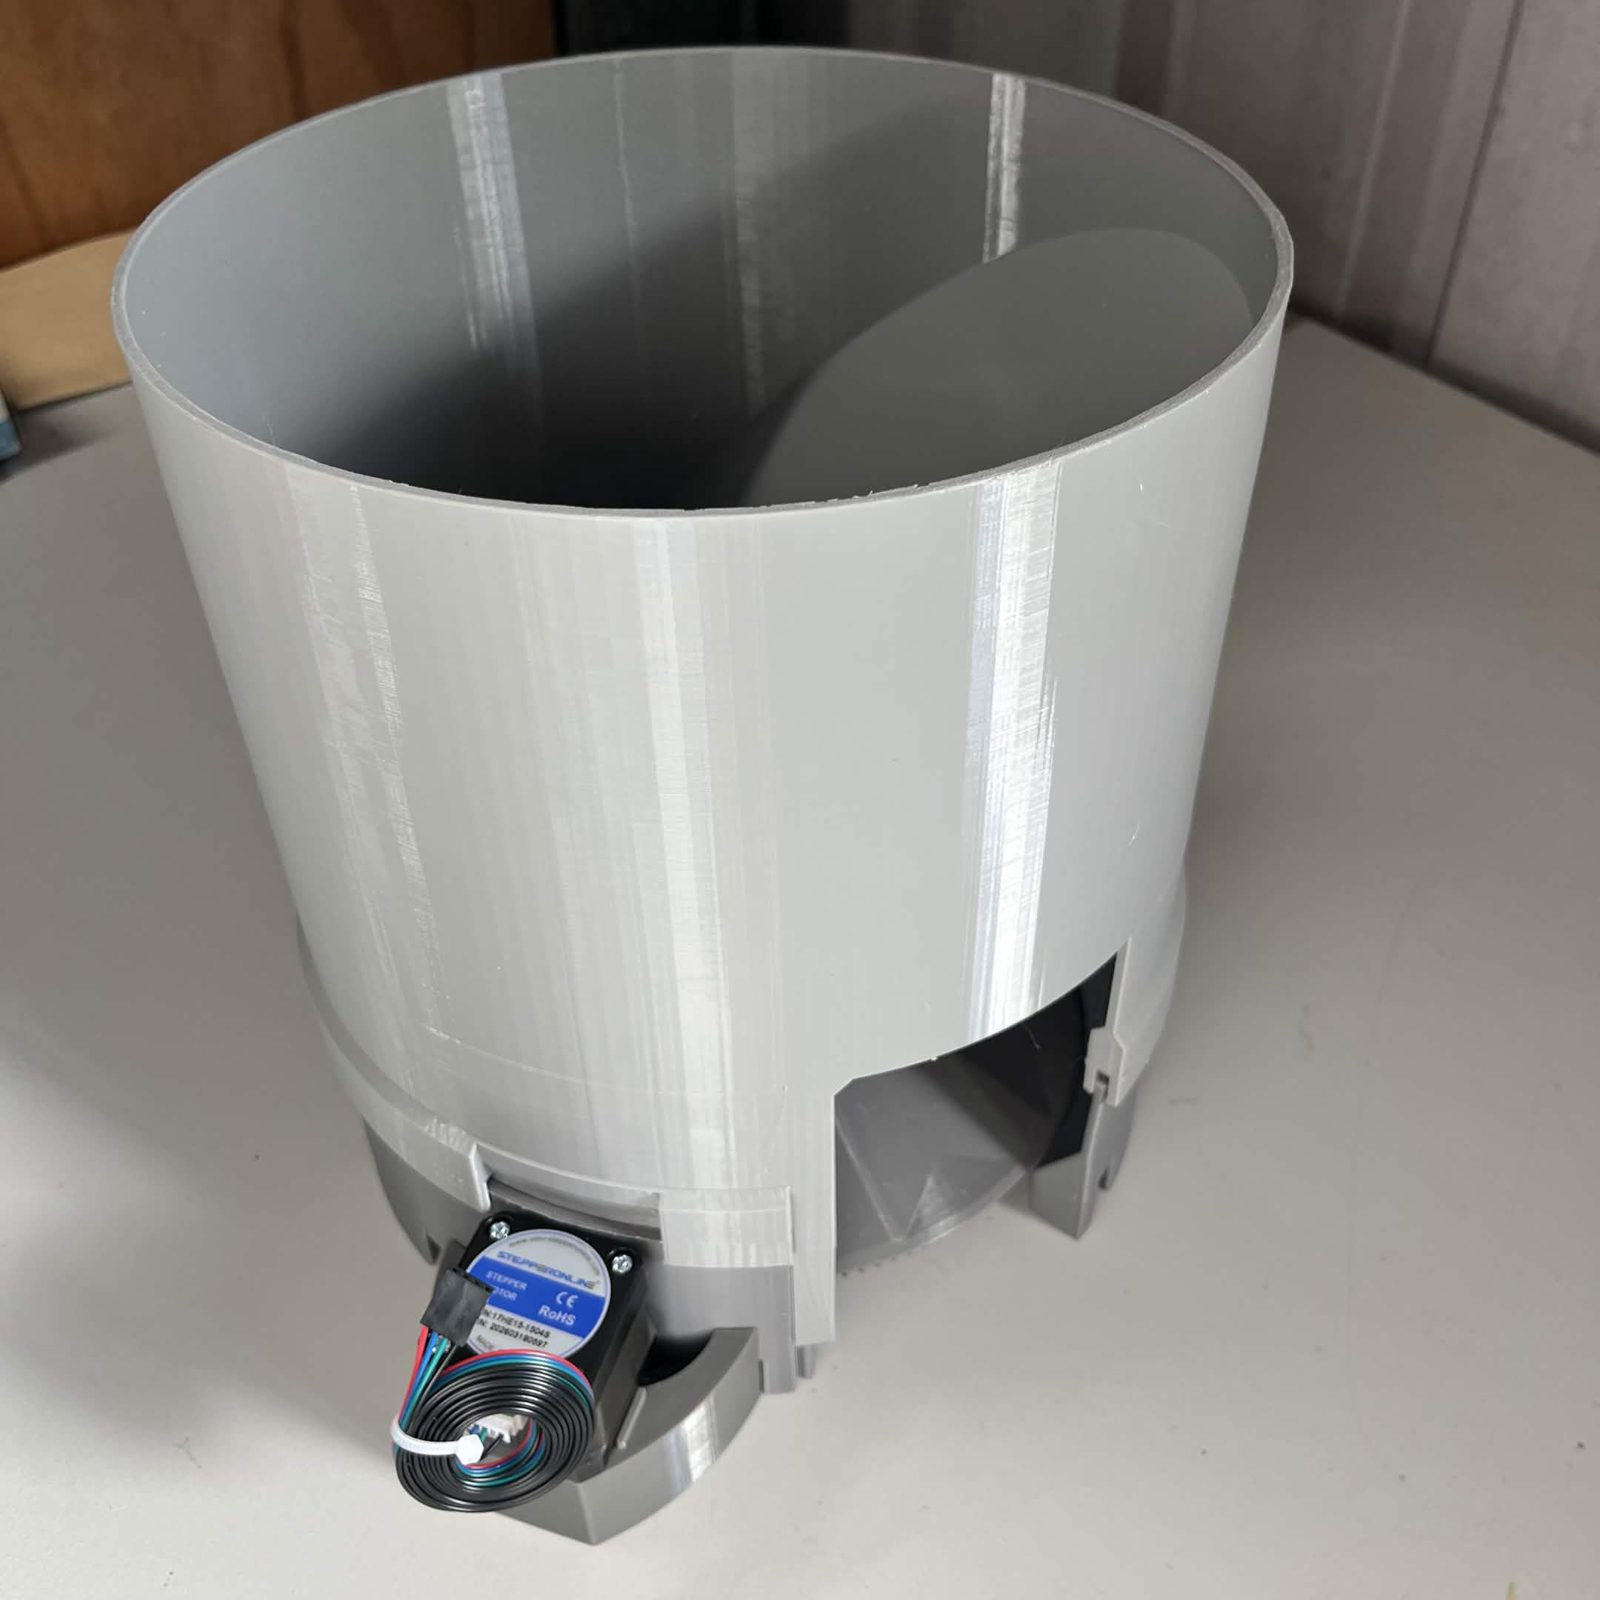
How-to guideThe top channel, where unsorted parts go in. The faceted rotor and the Bulk cap.
Parts needed
Printed parts
- 1×The feeder channels' rotor.
- 1×
- 1×
Bearings
- 1×
Screws
- 6× 12mm
Tools needed
- Hex key, 2 mm
Build a channel core before you start. This page turns one core into C1. It does not build the core.
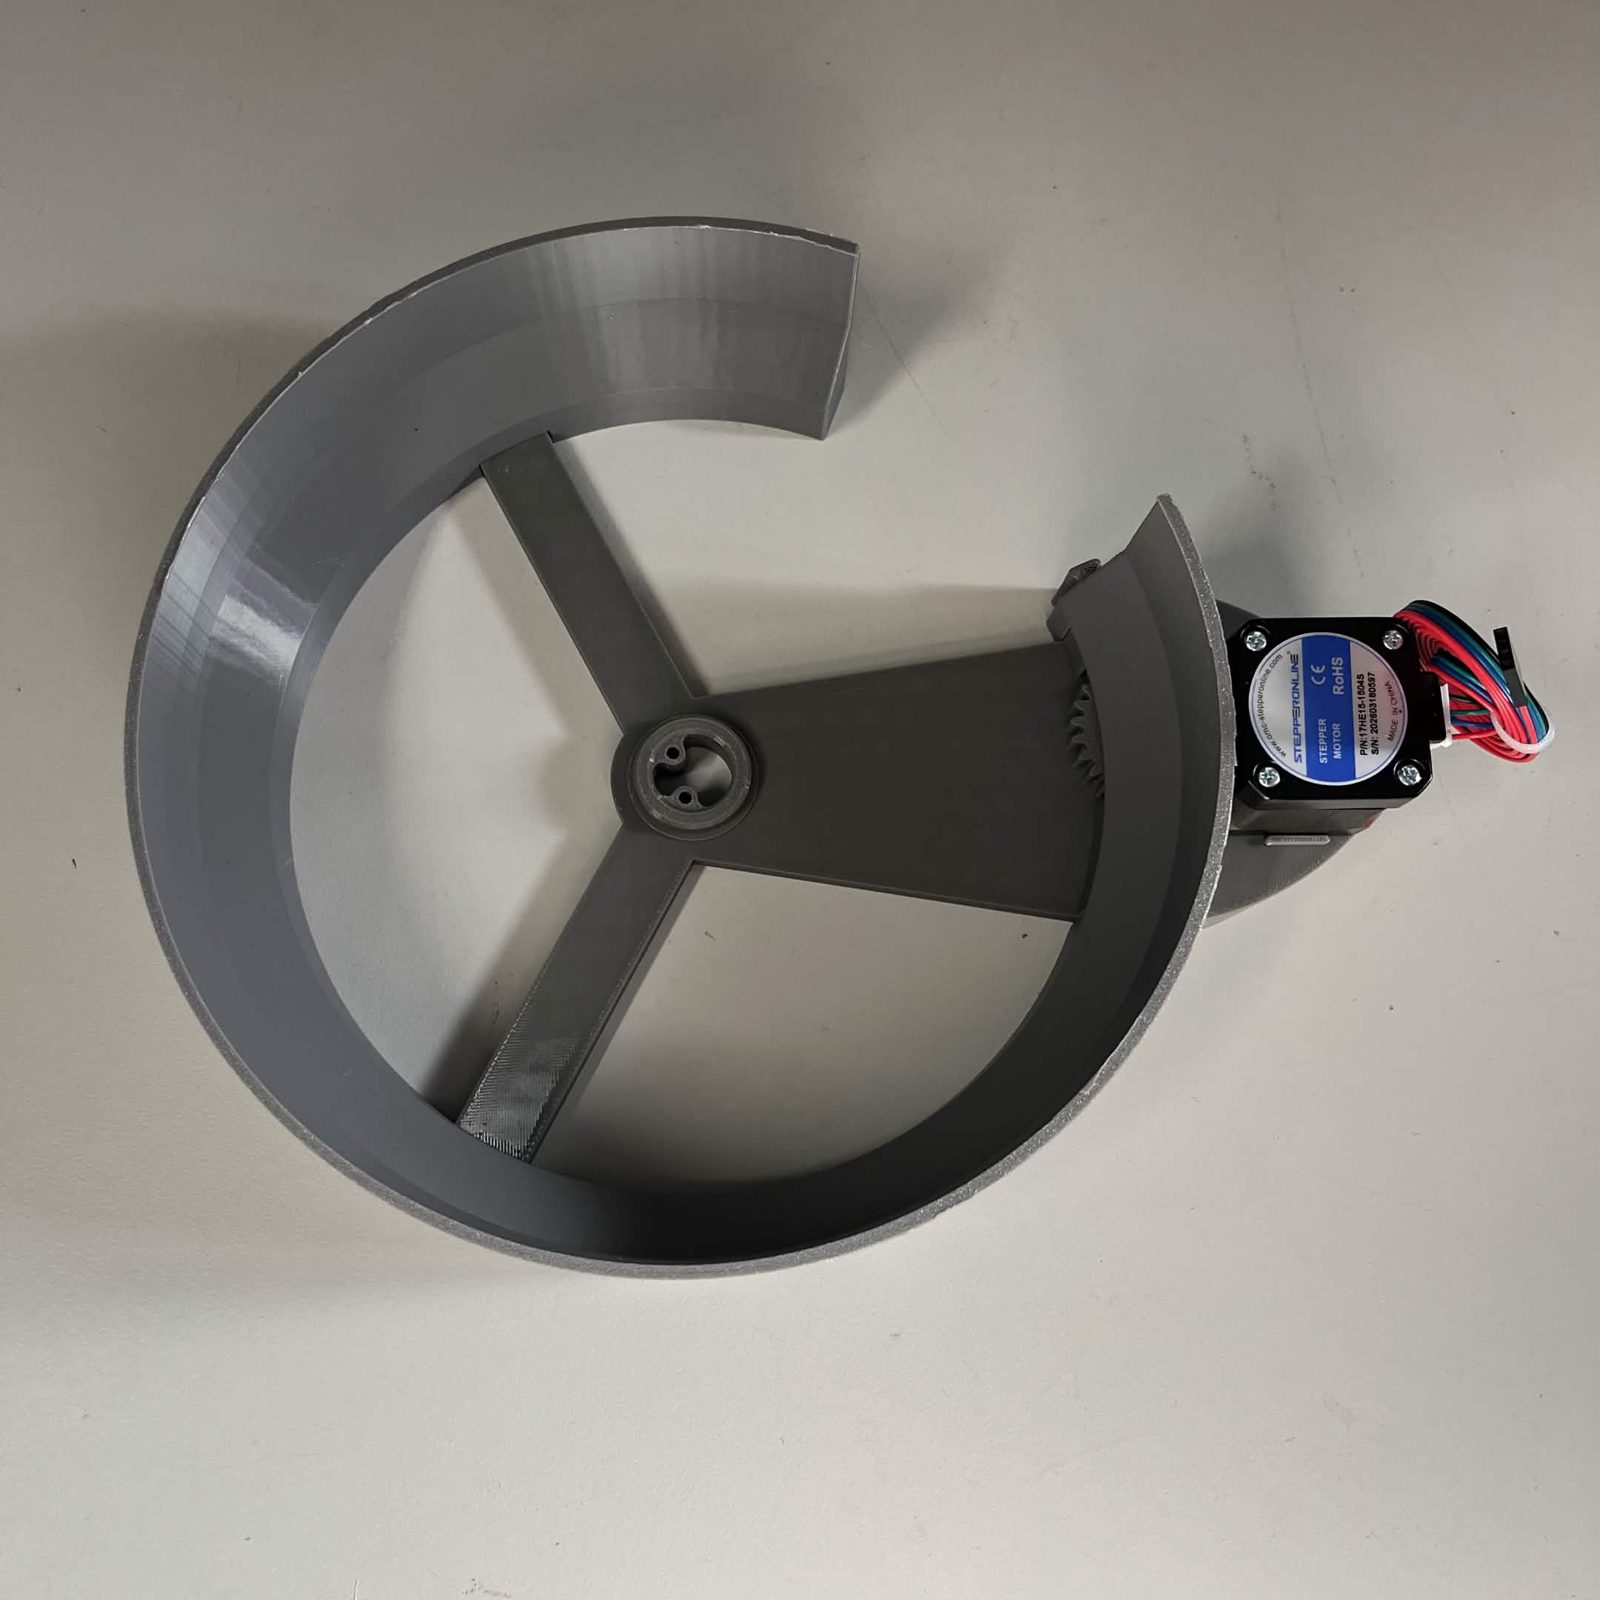
C1 is where unsorted parts go in. A bucket over the channel feeds them onto the rotor as it turns, and from here a part travels down to C2, C3 and the classification channel.
One per machine, the highest of the four. It takes the faceted rotor, like C2 and C3.
- No camera lamp and no output guide. The machine does not look at C1, and the Bulk cap has a guide built into it.
- The Bulk cap prints in the feeder colour.
Fastener icons match the parts list: the silhouette is the head shape, the colour is the thread size. M3 M4 M5 M6
Step 1 Preparation
Output gear (130T): press the 6806-2RS bearing into it. No screw, no glue, no heat.
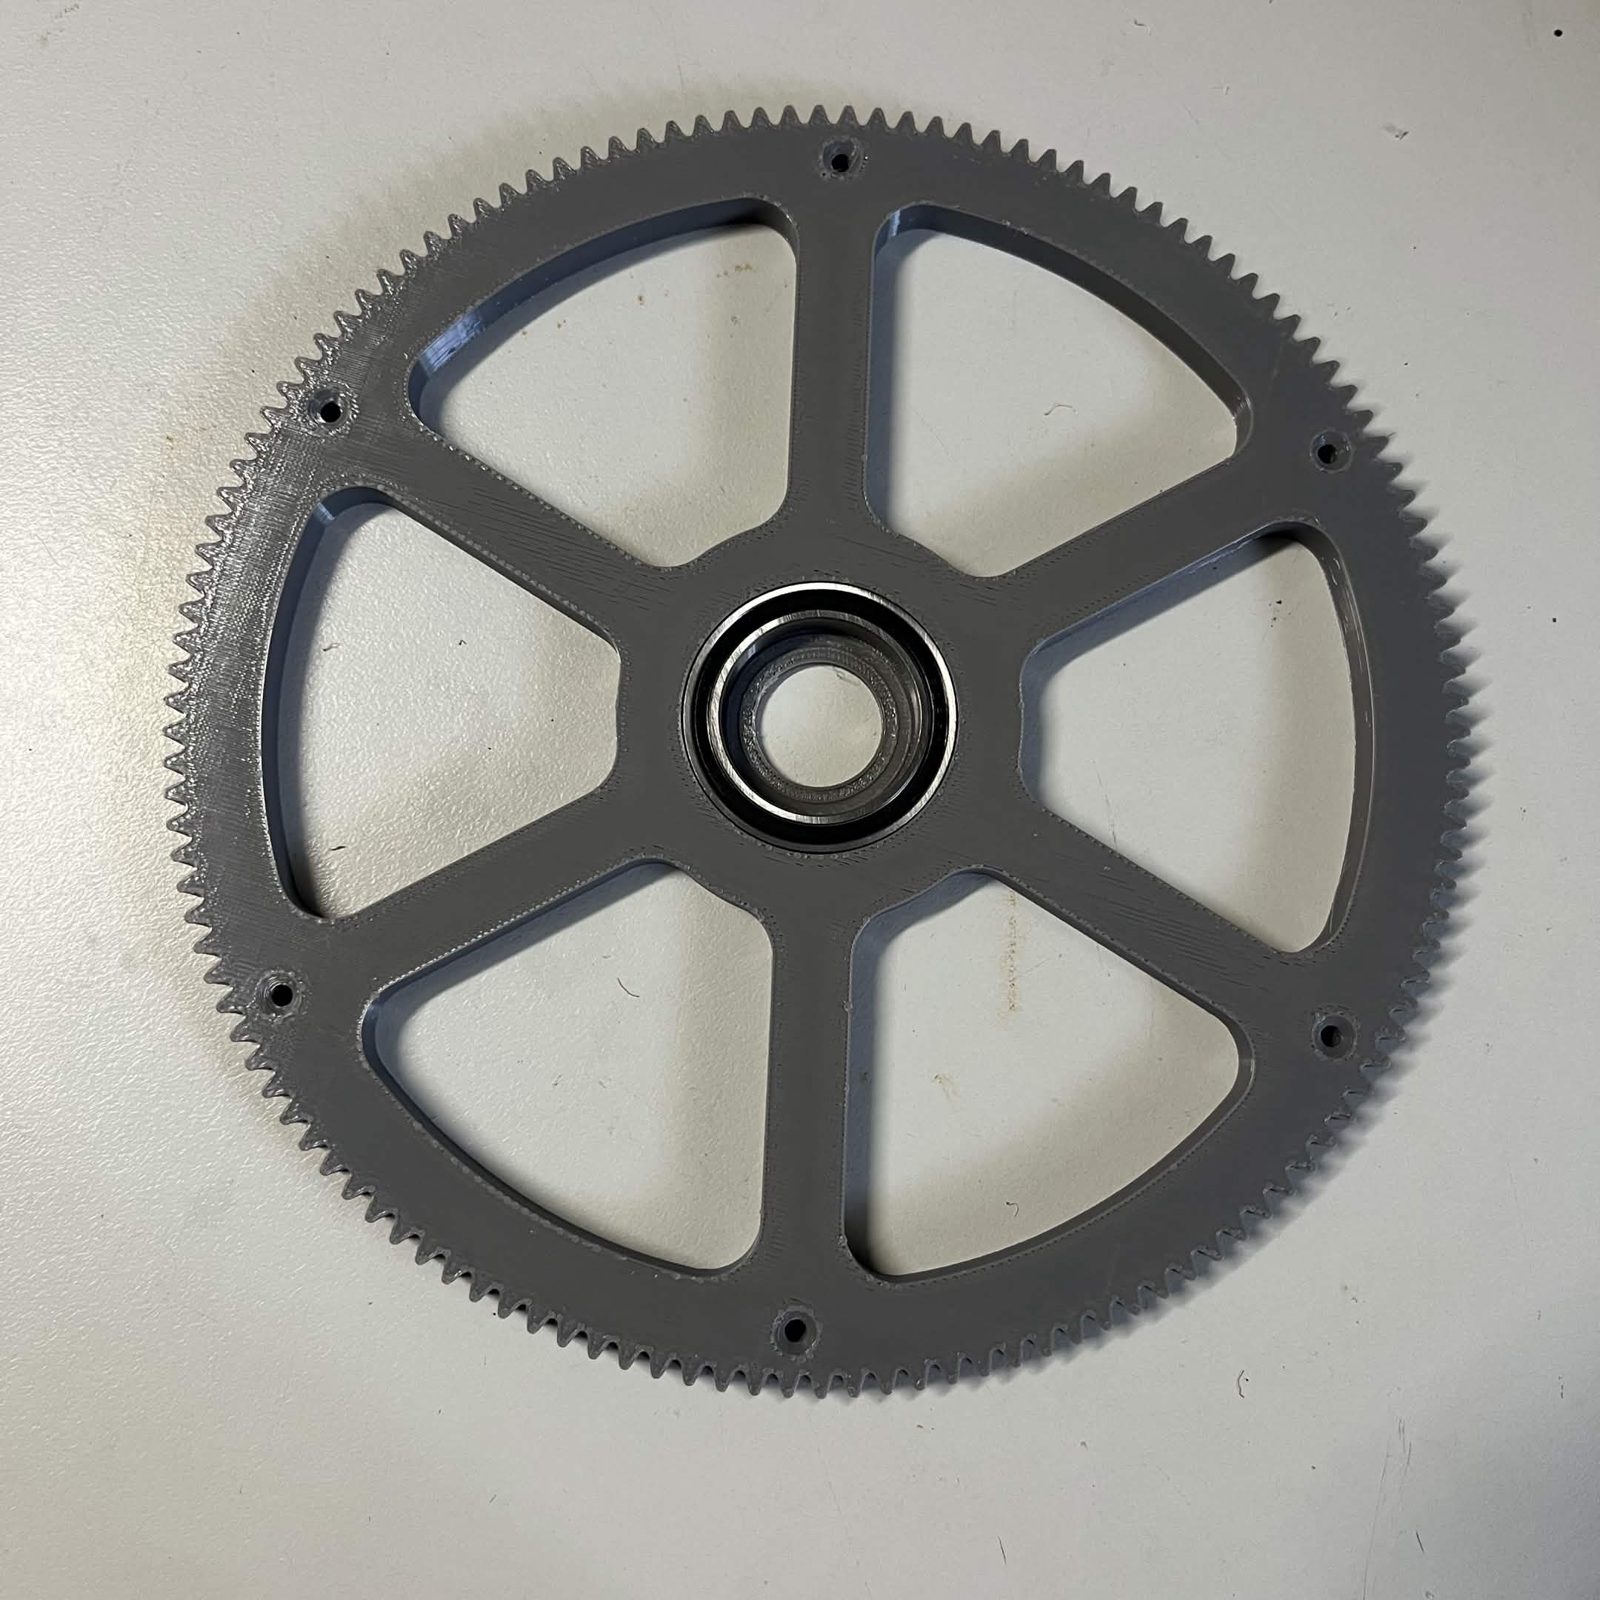
Step 2 Bolt the output gear to the rotor
The Output gear (130T) bolts to the open side of the Rotor (faceted).
- Turn the rotor so its open side faces up.
- Put the gear on it and line up the six holes. If it does not sit flat, turn it over.
- Drive one M3 × 12 mm countersunk screw at the outer end of each of the gear's six spokes, until the head is flush in the countersink.
It does not matter which way round you turn the gear. The six holes are the same all the way round.
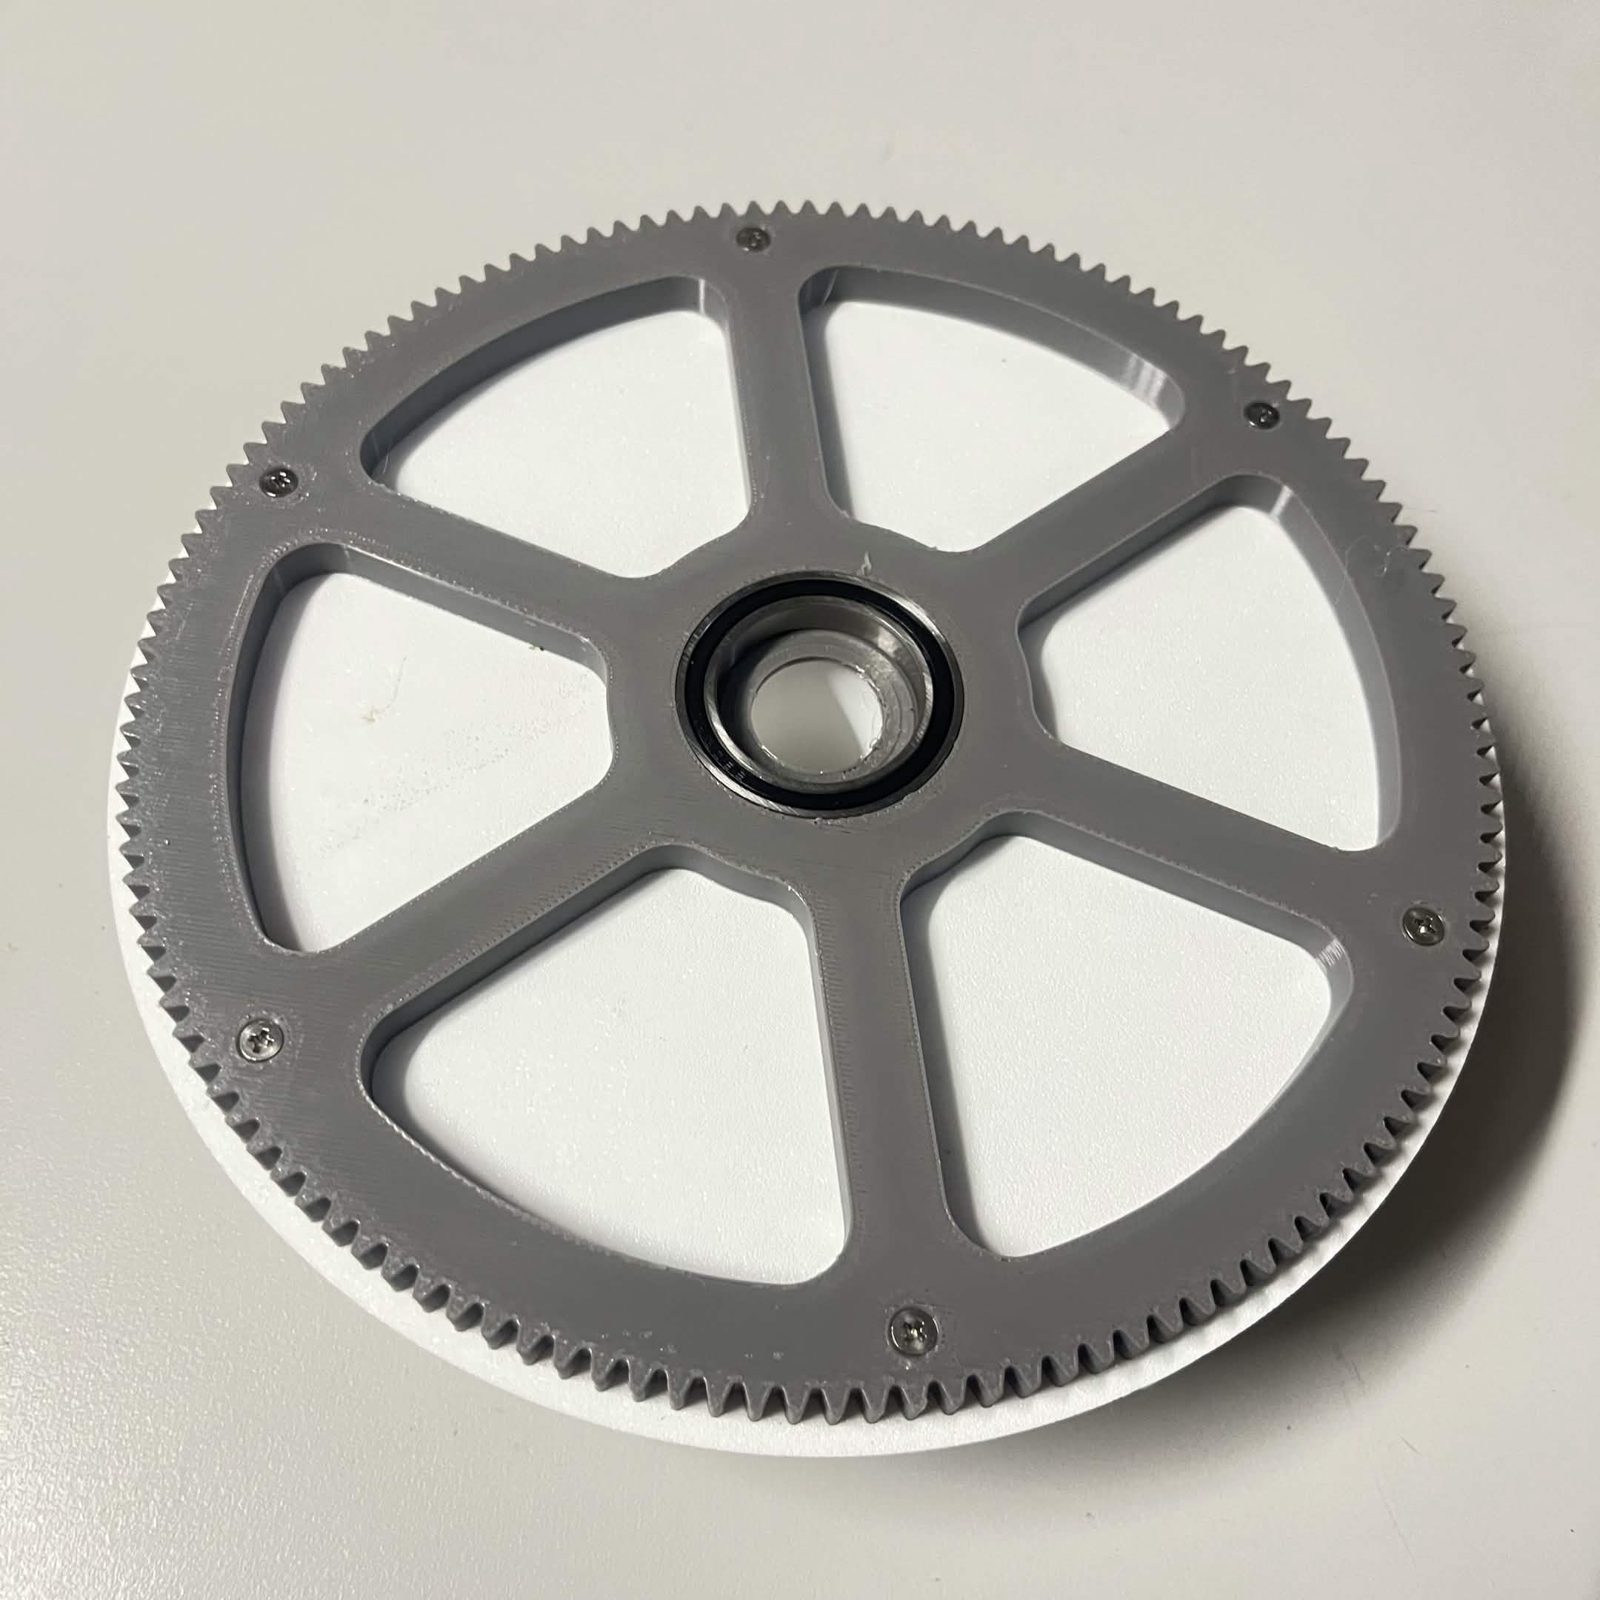
Step 3 Drop the rotor into the core
Lower the rotor onto the raised hub in the middle of the NEMA bracket. The output gear meshes with the idler as it goes down.
Turn the rotor by hand. It should go all the way round without a tight spot.
Step 4 Fit the bulk cap
Slide the Bulk cap down onto the dovetail on the outside of the stator wall. No screws. There is one dovetail on the stator, so there is one way it goes on; the channel's own clocking is set later, at arranging C-channels, step 4.
Use the current Bulk cap. The v1 dovetail needed too much force to slide on. If yours is a fight, check you have the latest file rather than forcing it.
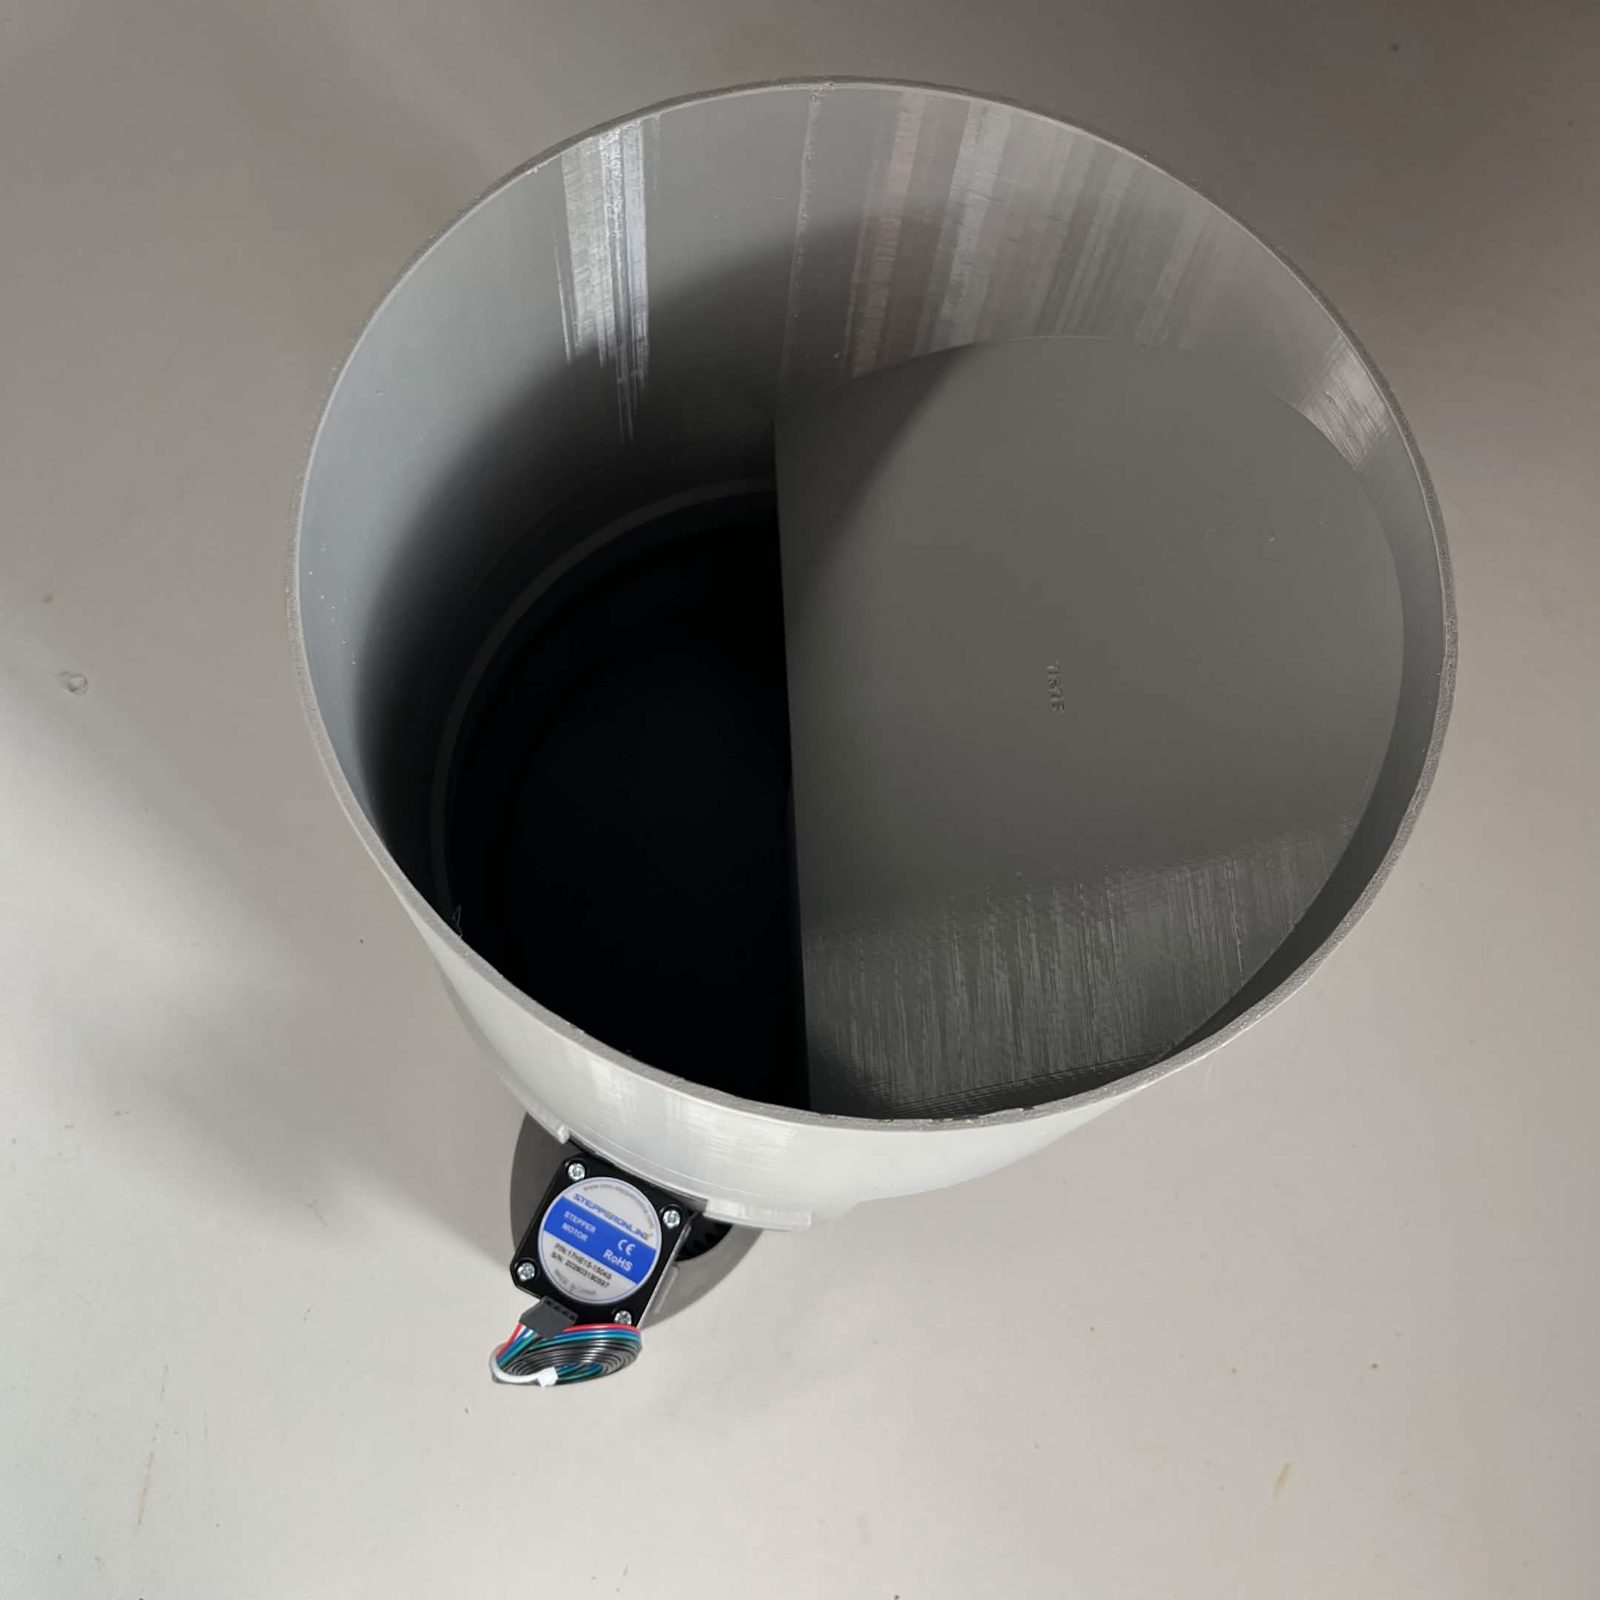
The finished result
A channel core with the faceted rotor in it and the Bulk cap on the stator. That is all of C1 that is documented: the bucket that goes over the cap is not published as a part yet. C1 stands at its height on arranging C-channels.
Back to C-channels.